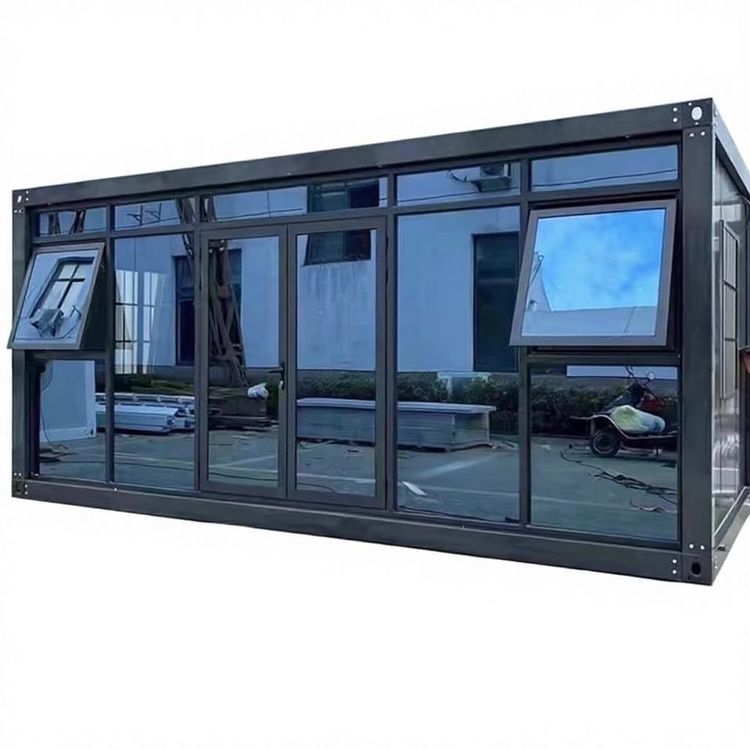
Guard Booth and Mobile Toilet Sheet Metal
The sheet metal processing of guard booths and mobile toilets involves core processes such as material selection, structural forming, welding techniques, and surface treatment, but specific technical requirements vary depending on the application scenario.

I. Key Technical Points for Guard Booth Sheet Metal Processing
Material Selection
The main structure of guard booths primarily uses cold-rolled steel sheets or galvanized sheets. The former is cost-effective and easy to process, while the latter enhances corrosion resistance through a galvanized layer. In special environments such as saline-alkali or humid conditions, some customized products adopt 304 stainless steel, which contains ≥18% chromium and ≥8% nickel, providing long-term resistance to oxidation and chemical corrosion.Forming Process
After being cut to size by a CNC shear, the steel sheet undergoes hydraulic bending. The bending radius is controlled by adjusting the mold angle (e.g., V-shaped or U-shaped molds) to prevent cracking caused by localized stress concentration. For example, when bending at a 90° angle, the radius is typically 1-2 times the thickness of the sheet.Welding and Inspection
Carbon dioxide gas shielded welding (CO₂ welding) or tungsten inert gas welding (TIG welding) is employed. CO₂ welding offers high efficiency but generates more spatter, while TIG welding produces aesthetically pleasing welds but at a higher cost. Welds are polished to remove burrs and inspected for internal defects (e.g., porosity, slag inclusions) using ultrasonic or radiographic testing to ensure structural strength. After welding, aging treatment (e.g., heating at 150-200°C for 2-4 hours) is performed to relieve residual stress and prevent deformation.Surface Treatment
The exterior is sequentially treated with phosphating (to form a phosphate protective film), sprayed with epoxy primer (for strong adhesion), and finished with polyurethane topcoat (for excellent weather resistance). Some high-end products incorporate a fluorocarbon coating (resistant to UV rays and self-cleaning). Electrostatic spraying ensures a coating thickness of over 80 microns, significantly exceeding the 30-50 microns of ordinary paint and greatly extending service life.
II. Key Technical Points for Mobile Toilet Sheet Metal Processing
Main Frame Material
High-quality manufacturers commonly use Q235 hot-dip galvanized square tubes (wall thickness ≥1.5mm) with a galvanized layer thickness of ≥65μm to resist corrosion in humid environments. The square tubes are welded or bolted to form a frame that must meet load-bearing requirements (e.g., the self-weight of a single-story toilet is approximately 1.5-2 tons).Functional Integration Design
The sheet metal structure must accommodate foam sealing, microbial degradation, or vacuum sewage systems. For example, vacuum sewage systems require reserved pipe interfaces and ensure sheet metal airtightness (leakage rate ≤0.5%) to prevent odor leakage. The ventilation system must provide ≥12 air changes per hour, achieved through sheet metal openings and fans.Customization Requirements
High-end mobile toilets feature irregular sheet metal cutting and assembly with streamlined exterior designs and internal equipment such as smart sensor faucets and air conditioners. The sheet metal thickness may increase to 2-3mm, with stiffeners added to enhance local rigidity for frequent relocation scenarios.
Summary: Guard booth sheet metal focuses on durability and aesthetics, while mobile toilets emphasize structural strength and functional integration. Both require strict process control to ensure consistent quality.
You may also like
Portable Toilet Eco-Friendly: MOQ, Samples & Quotation Guide
Read More
Top Portable Toilet Color Steel Manufacturers: How to Choose a Factory Partner
Read MorePortable Toilet Picture: Types, Features & Buying Tips
Read More