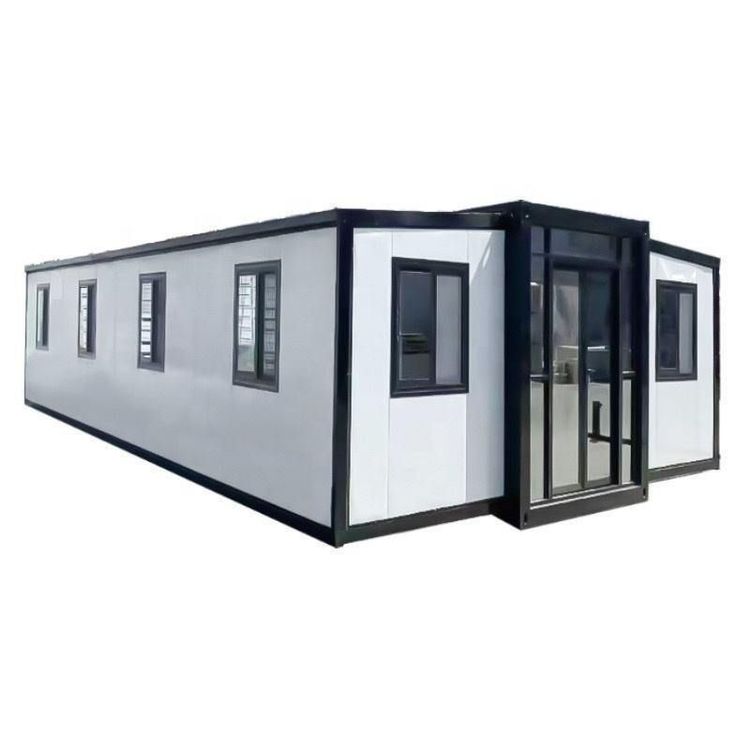
Container House Welding Tutorial
Welding a container house requires mastering key points such as material selection, frame welding, application of specialized equipment, and process control. The specific steps and precautions are as follows:
1. Material Selection and Frame Welding
The frame of a container house is composed of channel steel, square tubes, and columns. Channel steel (such as the 5×10 specification) is used to weld the main crossbeams around the top and bottom perimeters, similar to the ring beams of a house, ensuring firm welding to support the overall structure. The thickness of the columns should be no less than 1mm, usually requiring professional equipment for shaping or direct purchase of finished products from the market. Frame welding is crucial for the sturdiness of the house, requiring full and solid welds without cold welds to prevent deformation or breakage due to insufficient local strength.
2. Specialized Welding Machines and Process Applications
For different welding requirements in various parts, appropriate welding machines and processes should be selected:
- Front Wall Panel and Side Panel Welding: It is recommended to use the Megmeet Artsen II PM500F fully digital industrial heavy-duty MIG/MAG/CO2 welding machine, employing a direct current short-circuit process with specialized machine welding. This equipment can address issues such as unstable arcs, excessive spatter, and poor weld formation, especially suitable for thin plate welding, significantly improving surface flatness.
- Bottom Panel and Side Panel Welding: The Artsen Plus intelligent gas-shielded welding process platform should be used, utilizing a direct current short-circuit process to overcome the impact of anti-rust paint coatings on the arc, reducing weld defects and ensuring connection strength. Such processes are particularly important in high-end homestay renovations to prevent water leakage or structural cracking due to welding quality issues.
3. Welding Precision and Quality Control
- Structural Precision: The weld penetration, leg height, and diagonal errors of the box body should be strictly controlled. For example, CNC plasma cutting and fully automatic拼焊 (welding and assembling) processes can control the flatness error of the top and bottom frames within ±2mm, eliminating the risk of misalignment during lifting and assembly.
- Corrosion Protection: After welding, the entire box body should be galvanized or coated with epoxy zinc-rich primer to prevent weld corrosion during maritime transport or in humid environments. High-end manufacturers typically use automatic welding production lines certified by the International Institute of Welding (IIW) to ensure process stability.
- Thermal Performance: For homestay renovations, attention should be paid to thermal insulation and soundproofing. It is recommended to use basalt wool color-steel composite panels (with a thermal conductivity coefficient < 0.040W/(m·K)), which have a fire rating of Class A and maintain physical stability under extreme temperature differences.
4. Operational Specifications and Safety Precautions
Before welding, the oil stains and rust on the steel surface should be cleaned to avoid impurities affecting weld quality. During operation, protective gear such as face shields and gloves should be worn to prevent arc burns or injuries from spatter. After welding, the welds should be checked for uniformity and the absence of pores, and non-destructive testing (such as X-ray radiography) should be conducted if necessary to ensure internal quality.