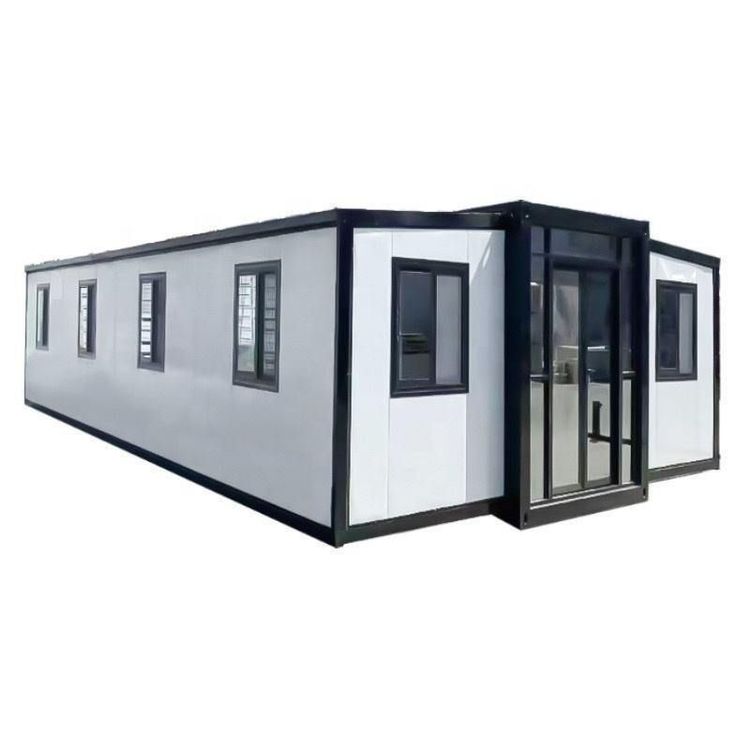
Container House Weld Standard
The weld standards for container houses are primarily based on the classification of weld quality levels, combined with the structural load-bearing characteristics and current regulatory requirements, and are specifically divided into the following aspects:

I. Classification of Weld Quality Levels According to the 'Code for Acceptance of Construction Quality of Steel Structures' GB50205, weld quality is divided into three levels:
- First-level welds: Require 100% flaw detection and are suitable for fully penetrated butt welds that directly bear dynamic loads (such as rigid beam-column connections, splicing of important tension members, etc.). These welds must be as strong as the base material to ensure the overall stability of the structure, such as at key locations like frame column splices and exposed column base connections between the column body and the base plate.
- Second-level welds: Suitable for butt welds that bear static loads (such as transverse or longitudinal butt welds, combination welds), usually undergoing 20% flaw detection. For example, fully penetrated butt welds of secondary members in multi-story steel residential buildings can be classified as second-level due to their relatively small loads.
- Third-level welds: Used for general fillet welds in non-critical load-bearing parts, requiring only visual inspection without flaw detection. For example, auxiliary welds in non-critical connection parts of container houses.
II. Special Requirements for Container Houses
- Structural Load-Bearing Characteristics: Container houses are primarily welded with section steel (such as channel steel, square tubes) as the main frame, with corner fittings being the only stacking load-transfer points. Spot welding is strictly prohibited as a substitute for continuous welds. The thickness of the main beam and column steel must meet design requirements (such as a column thickness of not less than 1mm), and the welding process must be full without cold welds, avoiding defects such as undercutting and incomplete fusion.
- Corrosion Protection and Durability: The weld area must undergo corrosion protection treatment (such as overall galvanizing or spraying) simultaneously with the base material to prevent rust from affecting structural safety. For example, the frames of standard container houses usually require surface protection after welding to extend their service life.
III. Relevant Standard Bases
- The 'Standard for Design of Steel Structures' GB50017-2017 clarifies the relationship between first-level welds and full penetration: key load-bearing parts (such as beam-column connections) must use fully penetrated first-level welds, but not all fully penetrated welds are first-level (such as secondary members can be second-level).
- The 'Acceptance Standard for Construction Quality of Container Houses' requires that weld quality must not only comply with the above standards but also meet material acceptance (such as steel and accessory quality) and factory production acceptance regulations to ensure full-process quality control.
IV. Practical Application Recommendations When purchasing or customizing container houses, it is essential to focus on checking whether the weld level matches the design load and request flaw detection reports. For multi-story or earthquake-resistant buildings with high requirements, structures with a high proportion of first-level welds should be prioritized to ensure safety and durability.