
Production Process of Cement Prefabricated Houses
The production process of cement prefabricated houses mainly includes four core steps: material preparation, mold making, pouring and curing, and assembly and transportation, integrating structural integration and new technology optimization.
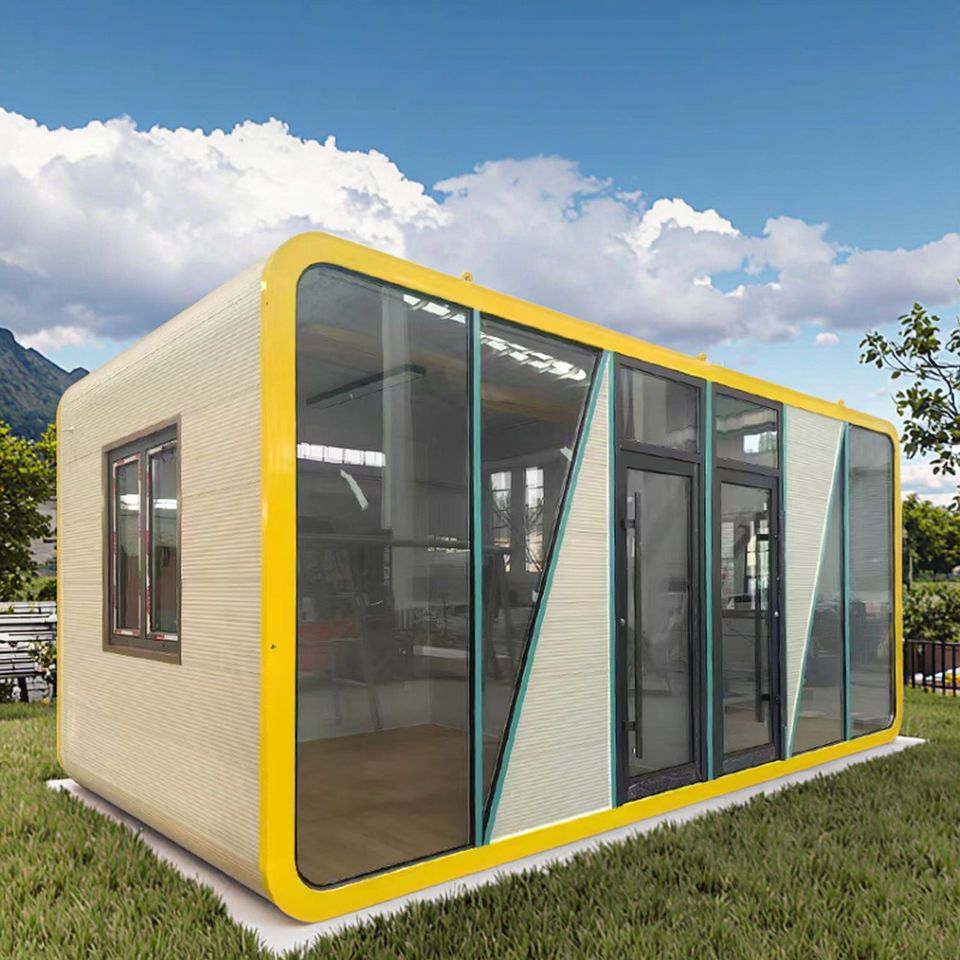
Material Preparation: Strict Control of Raw Material Performance and Testing
Material selection directly affects the quality of components. Cement should use P.O42.5 ordinary Portland cement, with strength and soundness meeting standards; sand should be medium-coarse sand, with a mud content of ≤3% to avoid affecting concrete adhesion; crushed stone particle size should preferably be 5-20 mm accounting for 60%, facilitating prefabricated part forming. Steel bars mostly use HRB400 deformed steel bars, with diameters selected from 8-14 mm according to load-bearing requirements, ensuring structural load-bearing capacity. All materials should be sampled and tested before entering the site: cement should undergo a soundness test, sand and gravel should be tested for gradation, and steel bars should be checked for tensile strength, ensuring material performance from the source.
Mold Making: Precision and Functionality Combined
Traditional wooden molds are gradually being replaced by steel molds. Factories commonly weld 5 mm thick steel plates into wall molds, with the inner walls brushed with release agents to prevent adhesion. Mold design should integrate multiple functions: internally embed water and electricity pipeline positioning devices, and fix plastic-steel frames at window positions for easy subsequent installation; construction personnel should verify that the diagonal deviation of the mold is ≤3 mm, and seal the corner joints with sealant to prevent slurry leakage affecting the surface quality of components.
Pouring and Curing: Process Control and Strength Guarantee
Before concrete pouring, a steel reinforcement cage should be arranged, with main bars and stirrups tied according to design drawings, and key nodes fixed with wire cross-ties. Concrete should be mixed using a forced mixer, with a water-cement ratio controlled between 0.45-0.5 to ensure a balance of fluidity and strength. The vibration rod should be inserted to the bottom of the mold, with each area vibrated for 20-30 seconds to eliminate air bubbles. After pouring, cover with plastic film for moisture retention. In winter construction, steam curing equipment should be activated to maintain an ambient temperature of ≥20°C. At normal temperatures, curing for 7 days can reach 70% of the design strength, and 28 days for full compliance; quality inspectors should test wall strength with a rebound hammer, and qualified components should be removed from the mold with a gantry crane and trimmed of flash and burrs.
Assembly and Transportation: Modularization and Structural Reinforcement
For transportation, special flatbed trucks should be used, with rubber pads installed between modules to prevent collisions. During on-site installation, the positions of foundation embedded parts should be verified, and walls should be connected to the foundation with high-strength bolts, with joints filled with special repair mortar. Specialized production bases use high-precision molds to pour core components such as walls and floor slabs in one go, integrating multiple structures including steel reinforcement cages, insulation layers, waterproof layers, and pipeline embeddings. Using C30-C40 grade concrete, with built-in Φ8-Φ12 steel bar meshes, the compressive strength reaches 25-30 MPa, equivalent to 1.5 times that of traditional brick-concrete structures; walls are pre-reserved with EPS insulation layer slots, with on-site embedding improving thermal insulation performance by 40%; modules are connected with prestressed bolts + welded steel plates, with a wind resistance rating of 10 and a seismic fortification intensity of 7 degrees. Some enterprises also attempt to add polypropylene fibers to the concrete to enhance crack resistance or use 3D printing technology to produce special-shaped components, further optimizing process performance.



